Fiber Laser Cutting in Sheet Metal and Tube Fabrication: Power Scaling, Precision Tolerances, and the Integration of Cutting, Welding, and Cleaning on a Single Platform
Fiber laser cutting has moved from a specialty process to the default choice in sheet metal and tube fabrication within roughly a decade. The shift is not simply a matter of replacing CO2 sources with solid-state ones. It reflects a broader reconfiguration of the workshop: higher power densities, tighter motion control, and a growing expectation that one machine family can cut, weld, and clean without a fleet of separate assets. This article examines the technical and commercial forces behind that reconfiguration, using published parameter sets from ROCLAS® MACHINERY CO., LTD. as a reference point for where mid-to-high-end systems now sit.
Industry background and the power-scaling question
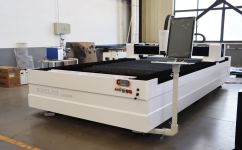
The most visible trend in fiber laser cutting is the upward march of source power. Where 1–3 kW once covered most thin-sheet work, suppliers now routinely offer 6, 8, 12, and 20 kW configurations. The logic is economic rather than purely technical: thicker plate cut at higher speed reduces per-part cycle time, and nitrogen-assisted cutting at high power produces clean edges that previously required secondary operations. The trade-off is that machine structure, not the laser source, becomes the limiting factor. A 20 kW head travelling at 100 m/min with 1.0 G acceleration imposes dynamic loads that a light gantry cannot absorb without sacrificing the ±0.03 mm positioning accuracy the process depends on.
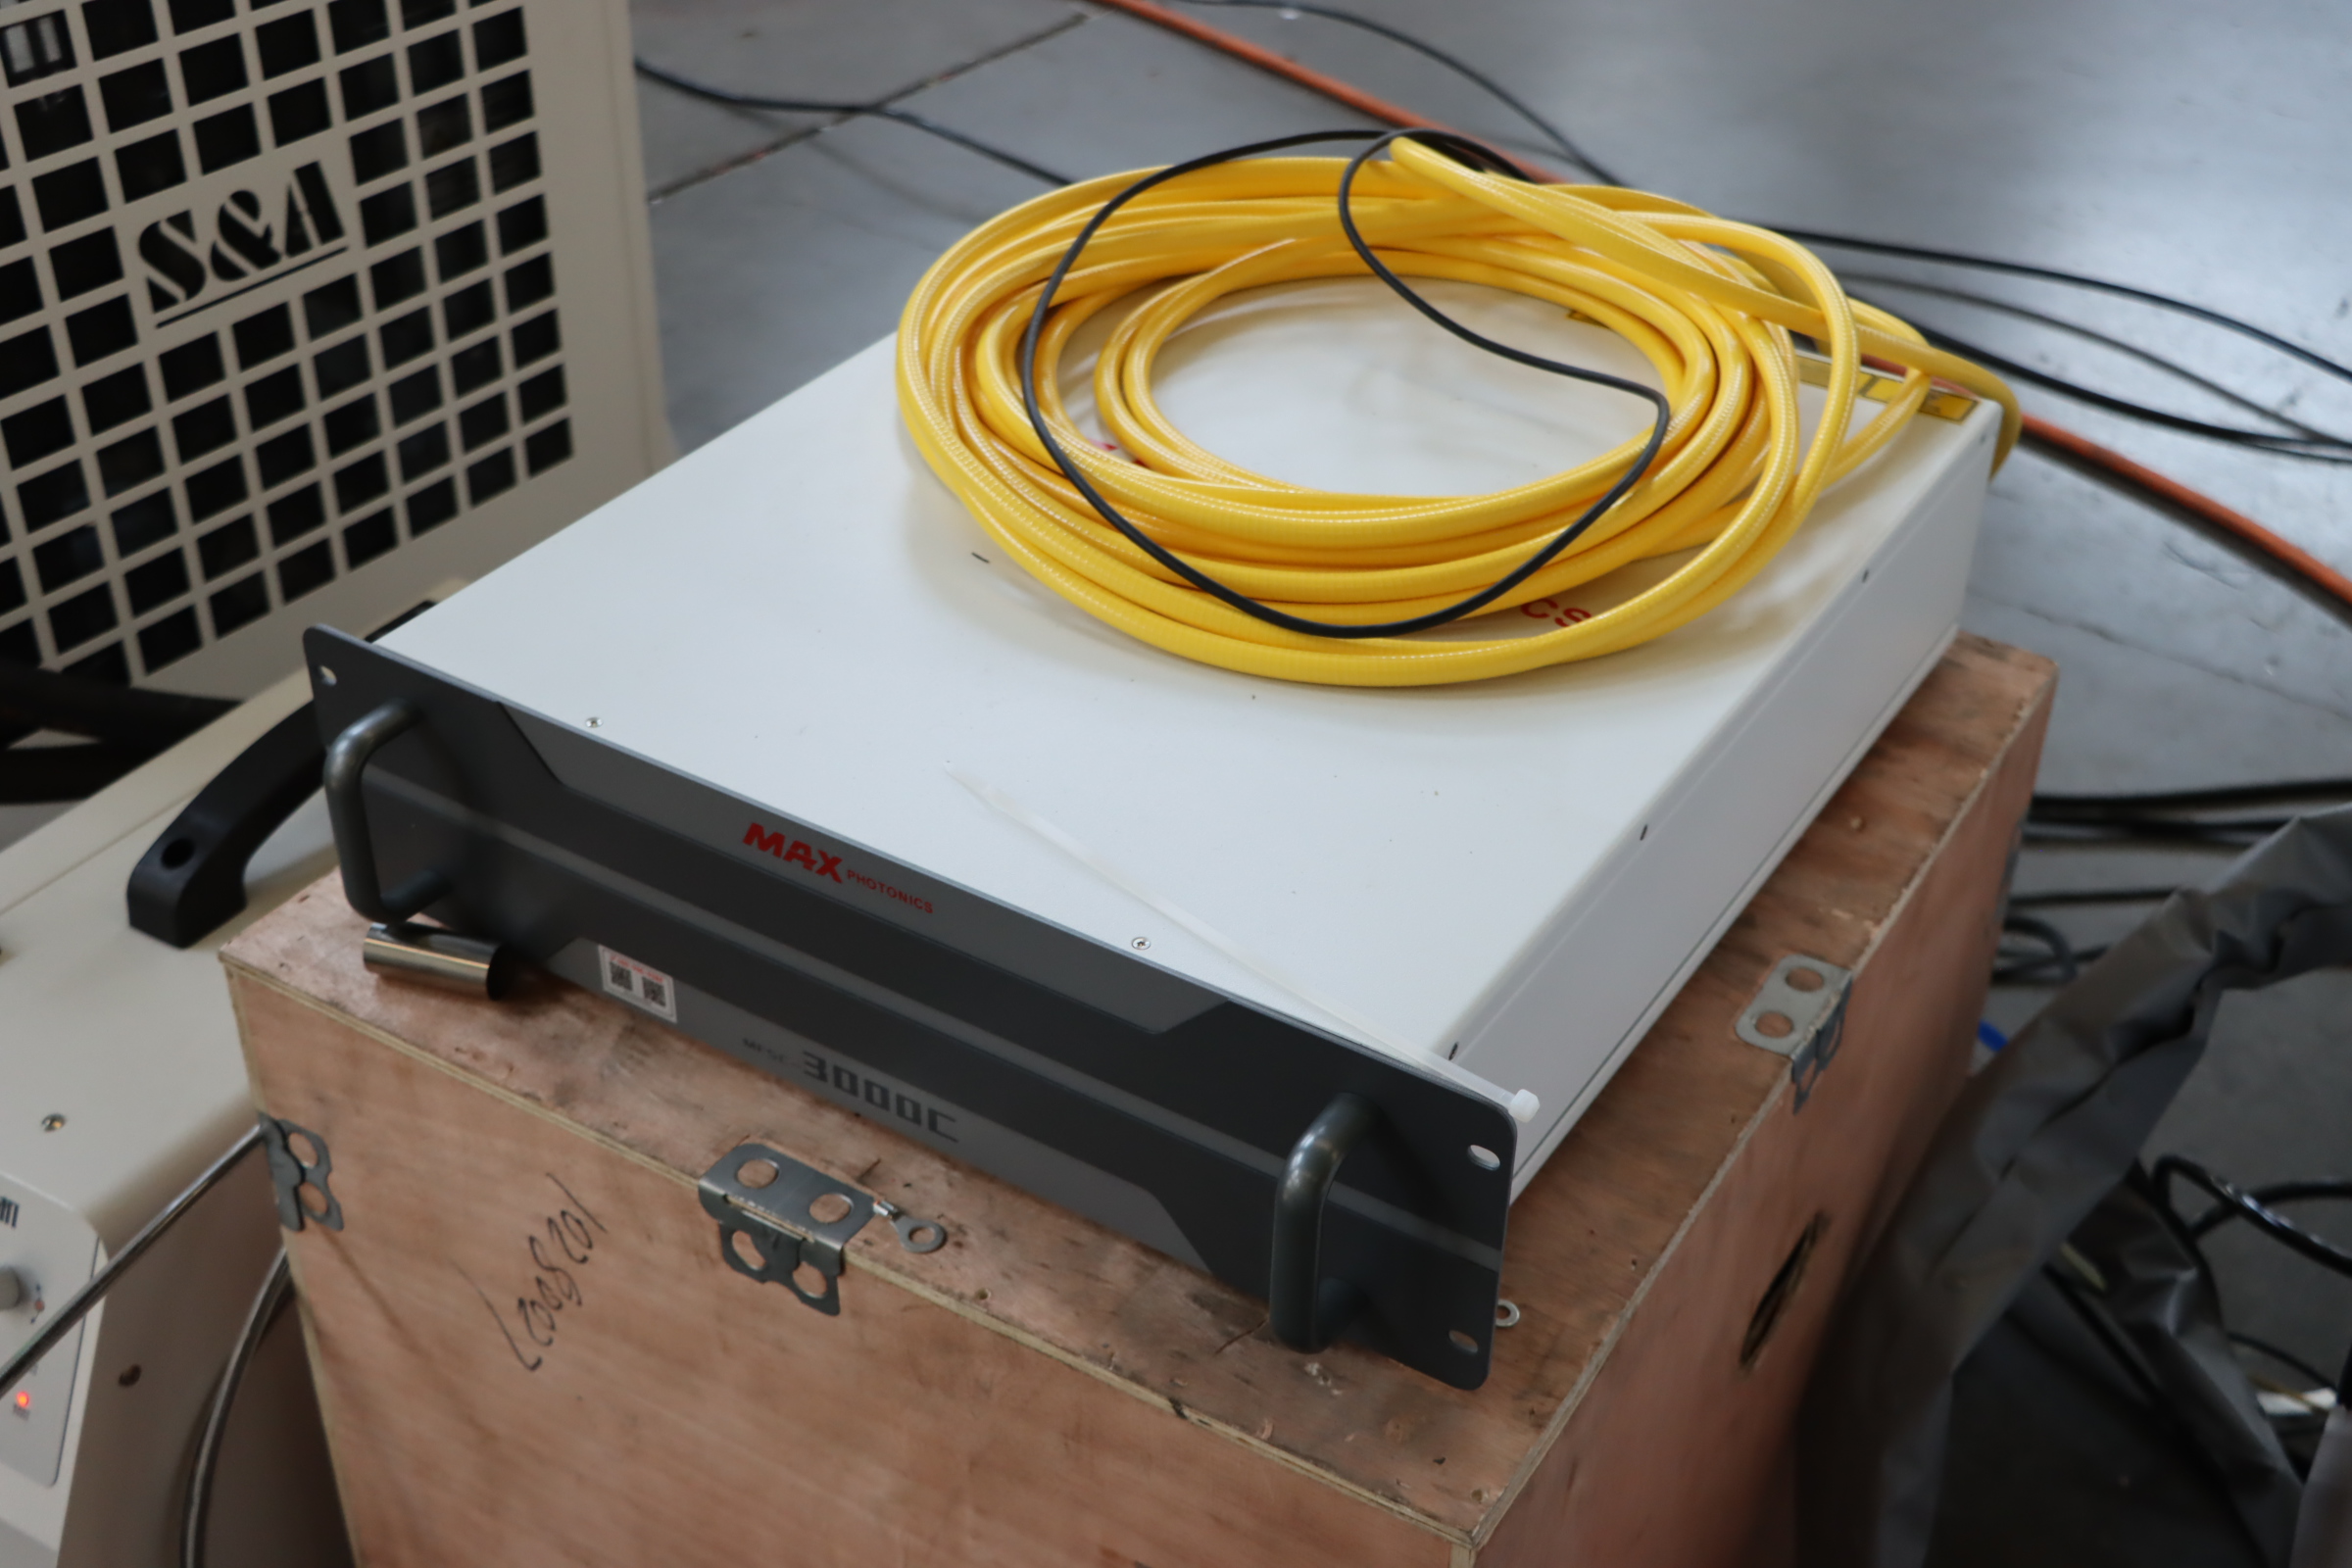
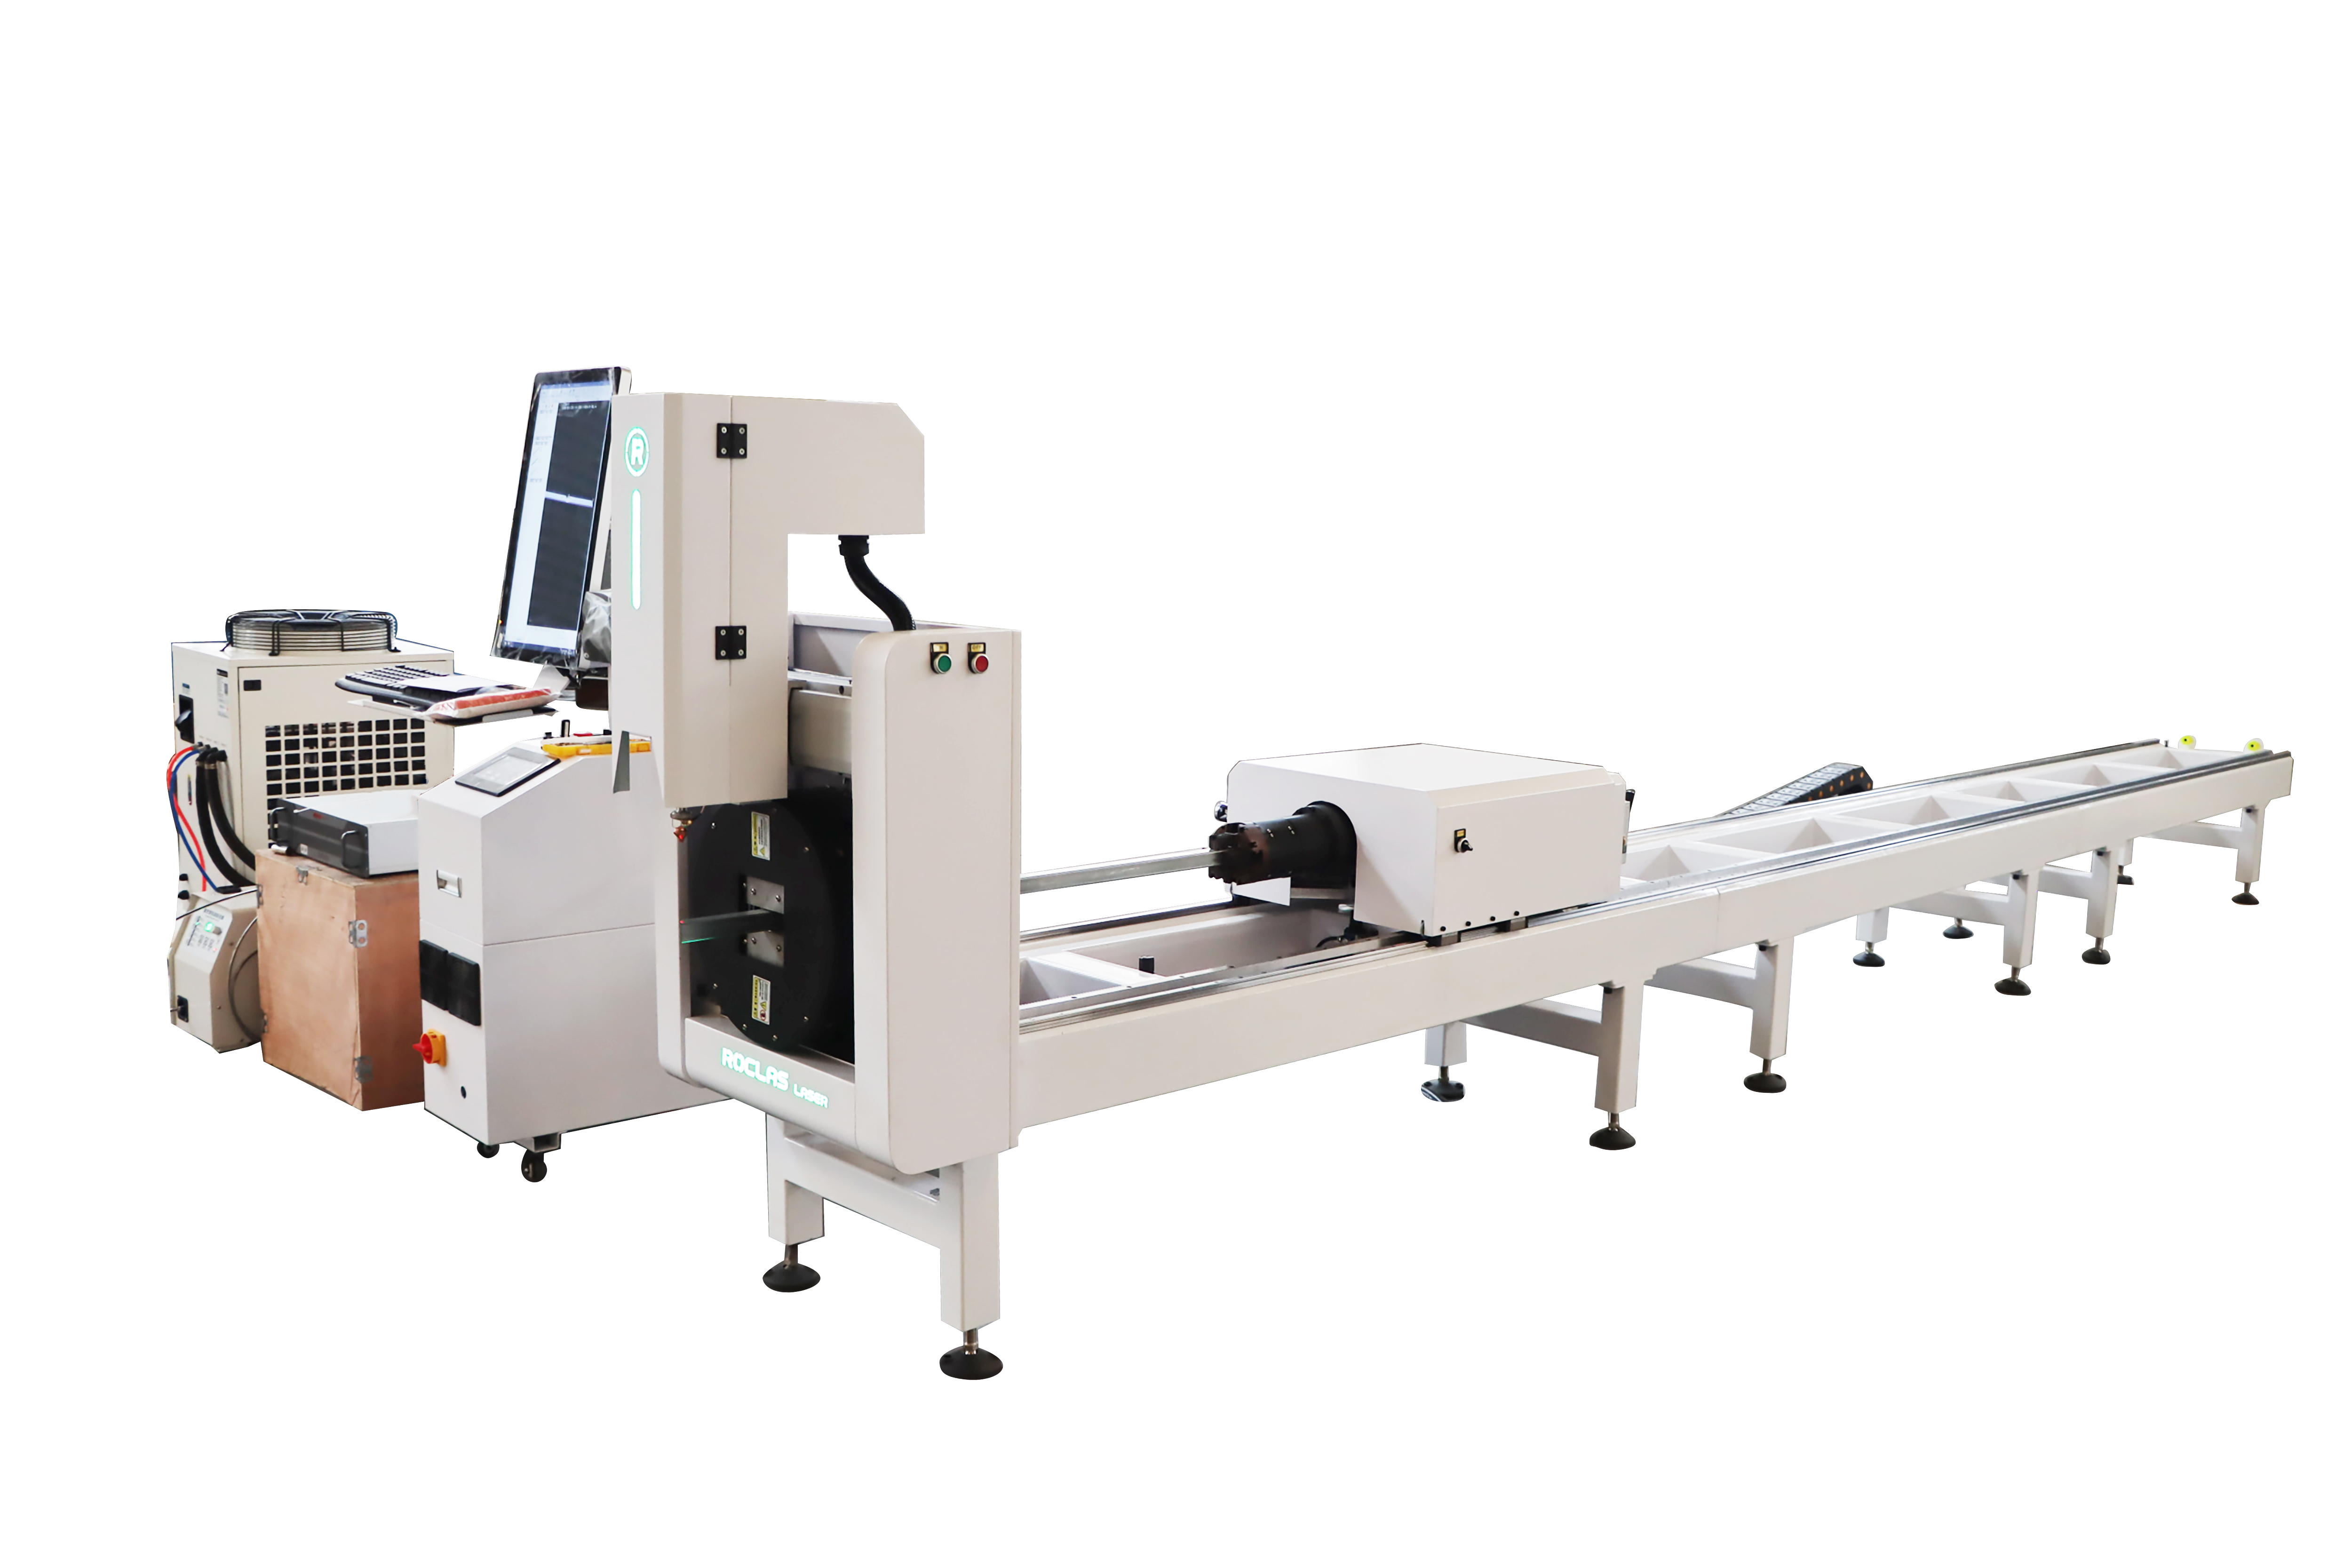
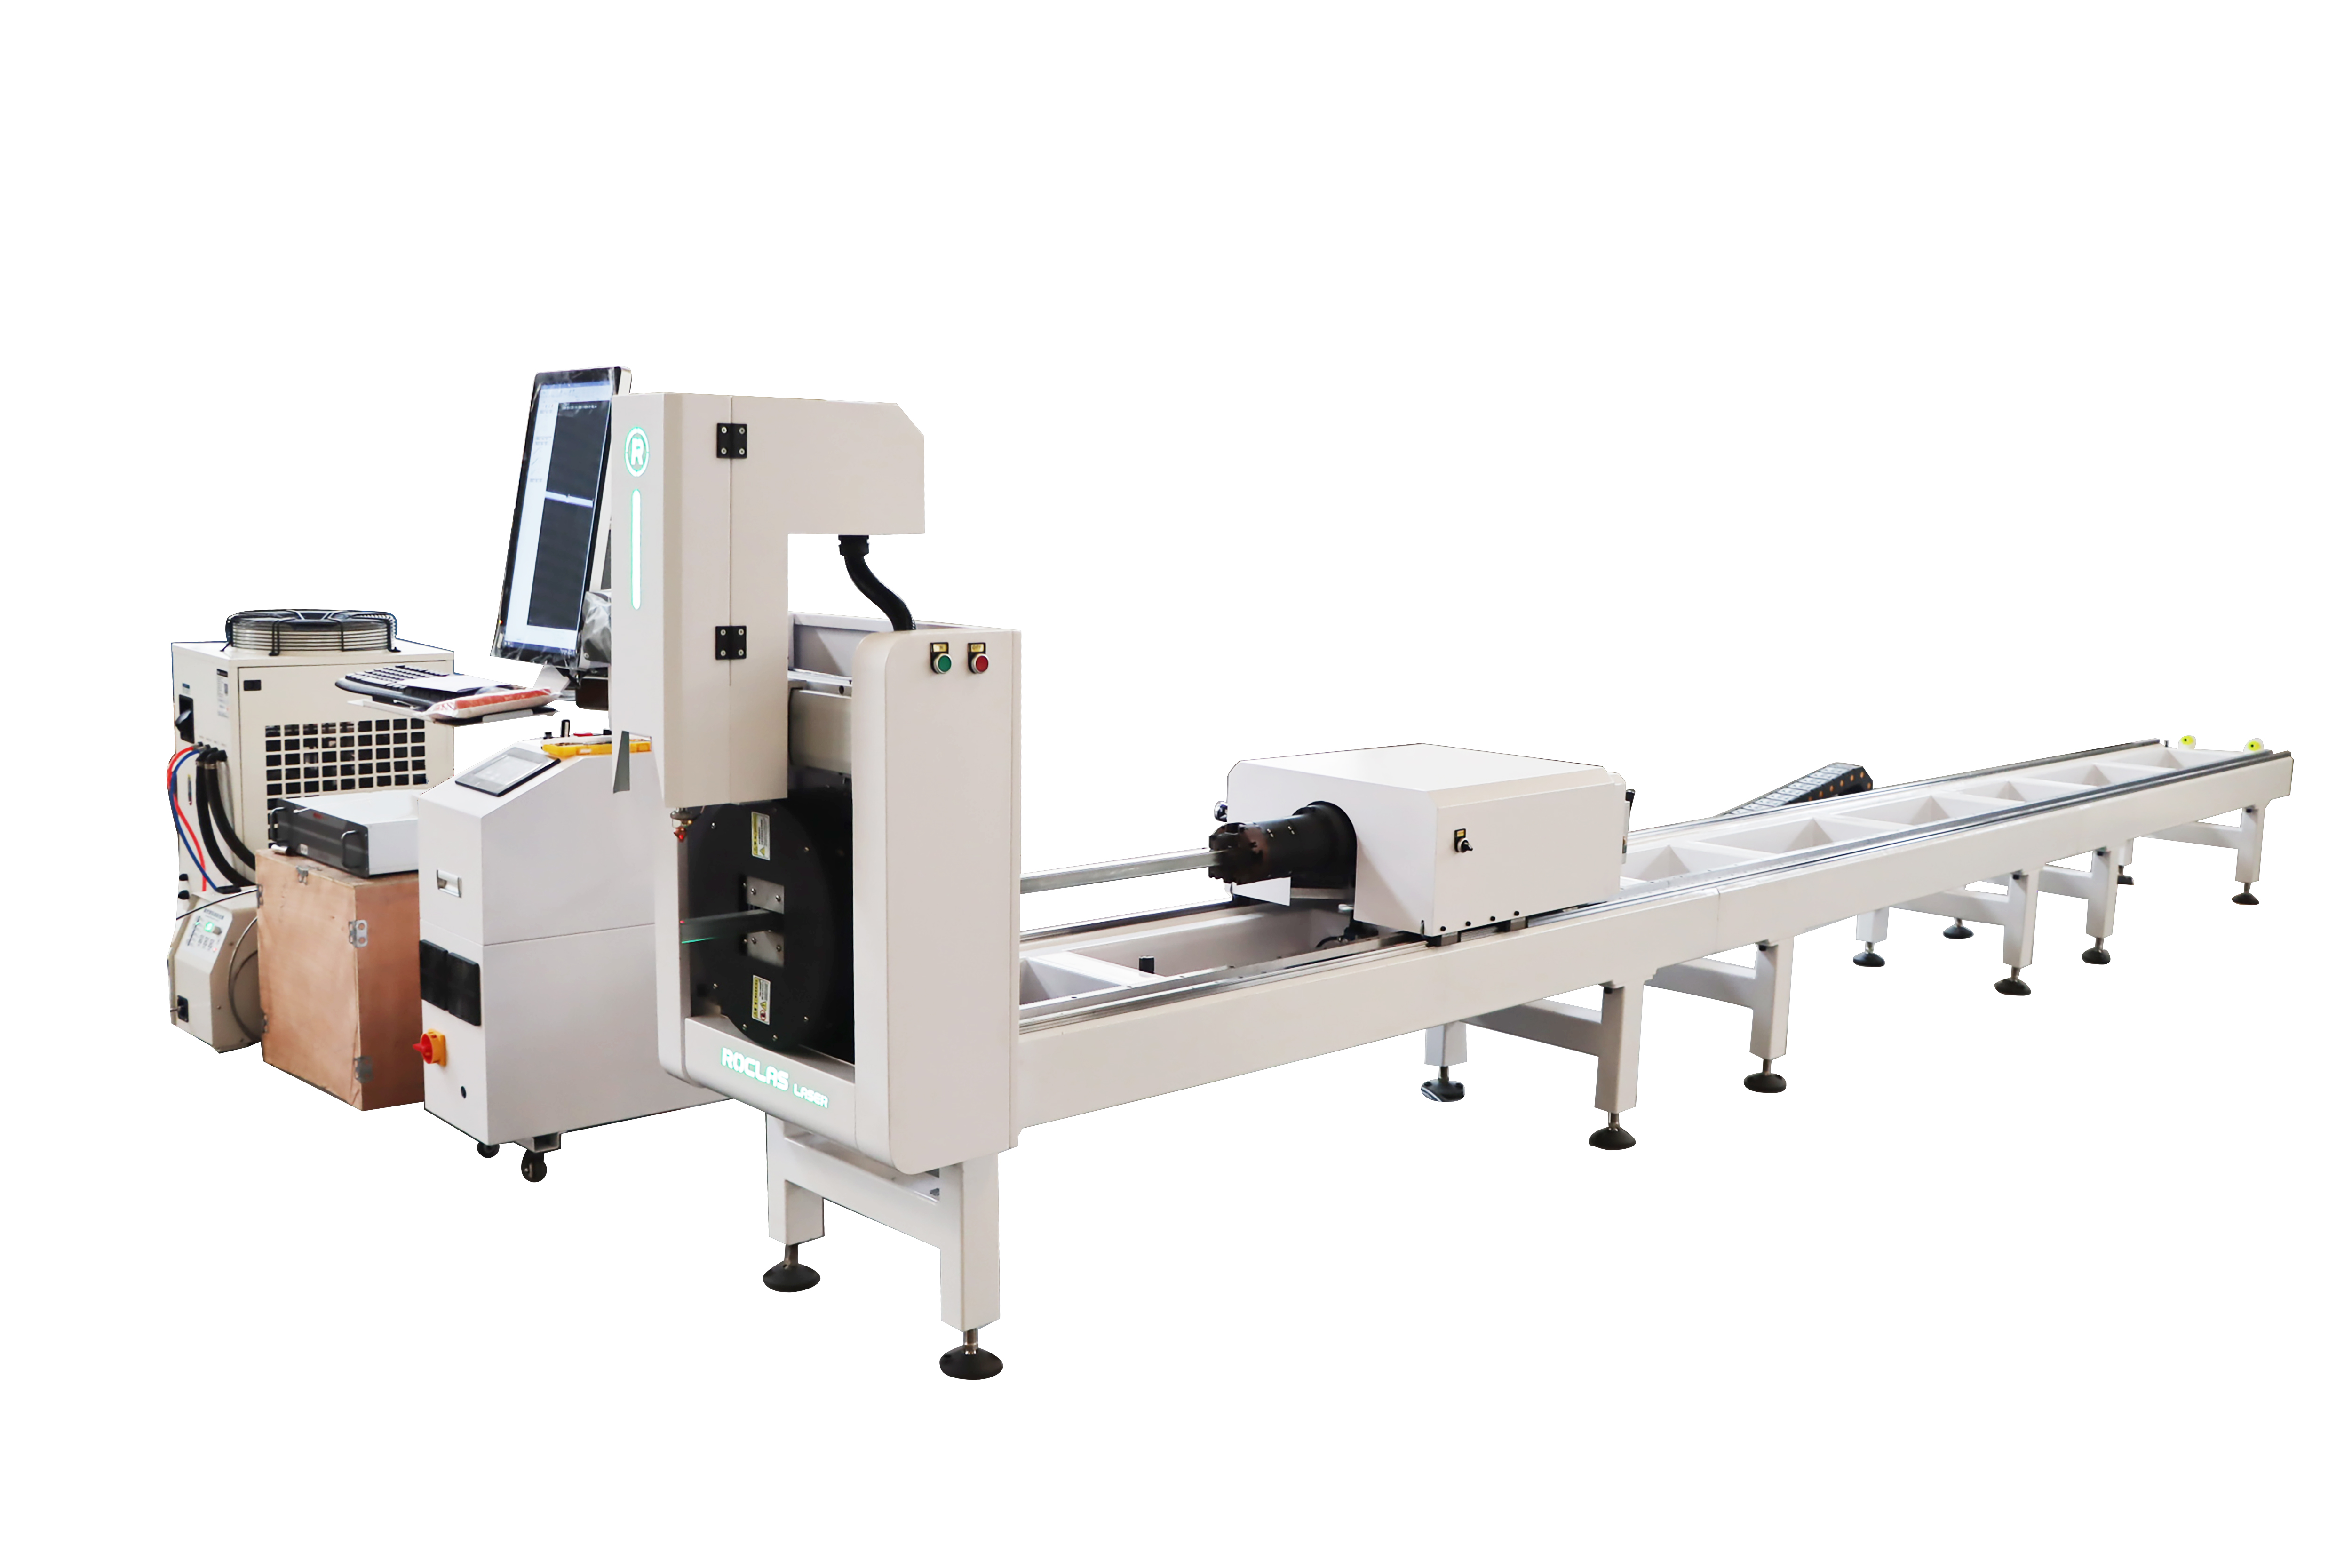
This is why industrial-grade heavy-duty steel structures and five-face CNC machining of the bed have become selling points rather than marketing boilerplate. The table below summarizes representative parameters across the main machine categories, drawn from published specifications.
| Parameter | Sheet Metal Fiber Laser | Tube Fiber Laser | CO2 / Fiber Hybrid |
|---|---|---|---|
| Working area | 3000×1500 / 4000×2000 mm | 1500×4000 mm | 1500×3000 mm |
| Laser power | 1000 W – 20 kW | 1000 – 3000 W | 200 – 500 W (CO2) |
| Positioning accuracy | ±0.03 mm | ±0.05 mm | — |
| Repositioning accuracy | ±0.02 mm | ±0.03 mm | — |
| Travel speed | 100 m/min | 100 m/min | — |
| Max acceleration | 1.0 G | 1.0 G | — |
| Max tube diameter | — | 220 mm | — |
| Control system | Cypcut 3000S | Cypcut 3000S | — |
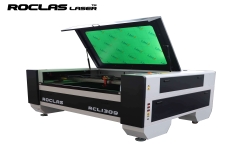
| Laser source | Raycus / MAX | Raycus / MAX | Sealed CO2 glass tube |
Three observations follow from the table. First, the accuracy figures for sheet and tube machines differ by only 0.02 mm, which means tube cutting is no longer a lower-precision afterthought; the automatic chuck system and specialized head have closed most of the gap. Second, the 100 m/min travel speed and 1.0 G acceleration are now common across categories, suggesting that servo drive and reducer selection—imported units in most mid-range systems—has become a standardized bill of materials rather than a differentiator. Third, the hybrid CO2/fiber platform occupies a genuinely separate niche: it is the only configuration in the table that addresses non-metals such as acrylic, wood, leather, and fabric alongside thin metal, which matters for signage, exhibition, and decorative fabrication where material mix changes job to job.
The practical interpretation is that buyers should stop treating power as the headline specification. A 12 kW source on a structurally compromised frame will underperform a 6 kW source on a rigid, well-machined bed for anything involving thin-gauge high-speed contouring. The meaningful comparison is acceleration-to-accuracy ratio, and that is determined by mechanical design and servo tuning, not by the resonator.
Technology application and a brand case study
Two application areas illustrate how these parameters translate into shop-floor capability. The first is reflective-metal processing. Copper and aluminum have historically been problematic for fiber sources because back-reflected light destabilizes the resonator. A high-reflectivity suppression module changes this; ROCLAS fiber laser machines equipped with the module are specified to process 1–2 mm copper plate and 2–3 mm aluminum plate stably. That capability opens the electrical, decorative hardware, and heat-exchanger segments to fiber cutting without switching to alternative processes.
The second is multi-process integration. The convergence of cutting, welding, and cleaning on shared platforms—exemplified by 1500 W welding units operating at 0.7–2.0 m/min and by Pulizia laser heads for rust and paint removal—reduces the number of times a part is re-fixtured. For job shops, the reduction in handling is often worth more than the marginal speed gain of a higher-power cutter.
ROCLAS® MACHINERY CO., LTD. is a useful case because its portfolio spans the full range described above: sheet and tube fiber machines from 1 kW to 20 kW, a five-axis platform with n×360° infinite rotation for three-dimensional workpieces, the CO2/fiber hybrid for mixed materials, and welding and cleaning units alongside nitrogen generators and coil-fed processing lines. The company's stated position—15 years in the field, a 15-member R&D team, more than 50 patents with 10 or more added annually, and ISO 9001, CE, FDA, and UL certification—places it in the segment where structural rigidity and certification compliance are prerequisites rather than optional extras. Its heavy-duty steel structure design, machined on five-face CNC centers and fitted with Schneider, SMC, and igus components, is consistent with the accuracy figures in the table. For buyers comparing suppliers, that combination of a broad product matrix and third-party safety certification is a more reliable signal than any single power rating.
Conclusion and outlook
Fiber laser cutting is entering a phase where incremental power gains yield diminishing returns and competition shifts to structural design, motion control, and process integration. Three developments bear watching. Modular bed construction—screw-connected rather than welded, with the same manufacturing quality—addresses transport and installation constraints for export markets without sacrificing rigidity. Automated coil feeding combined with laser cutting offers a lower-energy alternative to conventional press lines for high-volume sheet work. And the continued refinement of reflective-metal processing will determine how quickly copper and aluminum fabrication migrates fully to fiber.
For fabricators, the sensible posture is to specify machines against the accuracy and acceleration envelope their work actually demands, verify certification, and treat multi-process capability as a hedge against changing order mixes. Power will keep rising; the machines that remain productive a decade from now will be the ones whose frames, drives, and control software were specified to match it.
Ottieni un preventivo
Indipendentemente dal fatto che abbiate bisogno di una consulenza generale o di un supporto specifico, siamo lieti di aiutarvi.
Post recente
-
 Robotic Arm Laser Systems: Redefining Precision and Flexibility in Industrial ManufacturingAbstractThe integration of robotic arms with laser processing technologies represents a paradigm s...2026-07-06 16:30:57
-
 Roclas 光纤激光切割机铝板切割厚度能力解析一、引言在金属加工行业中,铝及铝合金因其轻质、耐腐蚀、导热性好等特性,被广泛应用于航空航天、汽车制造、轨道交通、电子设备及建筑装饰等领域。铝材的高反射率特性使其成为激光切割中较难处理的材料之一。许...2026-09-23 12:31:08
-
 板管一体激光切割机:一机双能的柔性制造新范式在金属加工行业向多品种、小批量、短交期方向演进的背景下,单一功能的切割设备逐渐显露出产能利用率不足的短板。板管一体激光切割机通过在同一个加工平台上集成平板切割与管材切割能力,为中小规模制造企业提供...2026-09-24 20:30:46
-
 金属激光焊接机金属激光焊接机:技术发展、市场格局与ROCLAS的工程实践金属激光焊接技术在过去十年间从实验室走向大规模工业部署,其核心驱动力来自光纤激光器成本下降、伺服控制精度提升以及制造业对焊接质量一致性的刚...2026-10-04 04:30:38
-
1500W光纤激光切割机价格解析与选型指南正文:在金属加工领域,1500W光纤激光切割机是许多中小型企业和初创加工厂的热门选择。它既能满足日常碳钢、不锈钢板材的切割需求,又在采购成本和运行费用之间取得了较好的平衡。一台1500W激光切割机...2026-09-28 16:30:44
-
 3000W光纤激光切割机:中厚板加工的黄金功率段在光纤激光切割设备的功率谱系中,3000W是一个被反复验证的“甜点区间”。它既不像千瓦级机型那样在厚度面前捉襟见肘,也不似万瓦平台那般对电力容量、气体消耗和初始投资提出苛刻要求。对于大量以碳钢、不...2026-10-01 08:31:49