Fiber Laser Cutting in Sheet Metal Fabrication: Power Scaling, Precision Limits, and the Integration of Cutting, Welding, and Cleaning on a Single Platform
Abstract
Fiber laser cutting has moved from a niche alternative to the default process for thin- and medium-gauge sheet metal within less than a decade. The transition has been driven less by any single breakthrough than by a steady convergence of higher source power, tighter motion control, and better beam management at the cut front. What matters to fabrication shops today is not the headline wattage on a specification sheet but whether the machine can hold tolerance across a full shift, process reflective alloys without interruption, and absorb secondary operations such as welding and surface cleaning without a second capital purchase. This article examines the current state of fiber laser cutting through the lens of machine architecture, published performance parameters, and the practical experience of equipment builders operating in this segment.
Industry Background and Data Analysis
The economics of sheet metal fabrication have shifted decisively toward laser-based separation. Plasma and punching retain roles in thick plate and high-volume hole work respectively, but for mixed-batch production the fiber laser has become the reference tool. The reasons are structural: fiber sources convert electrical energy to optical output at considerably higher efficiency than CO2 tubes, require no laser gas, and deliver beam quality that supports narrow kerfs and small heat-affected zones. The downstream consequence is lower cost per part and, just as importantly, less post-cut finishing.
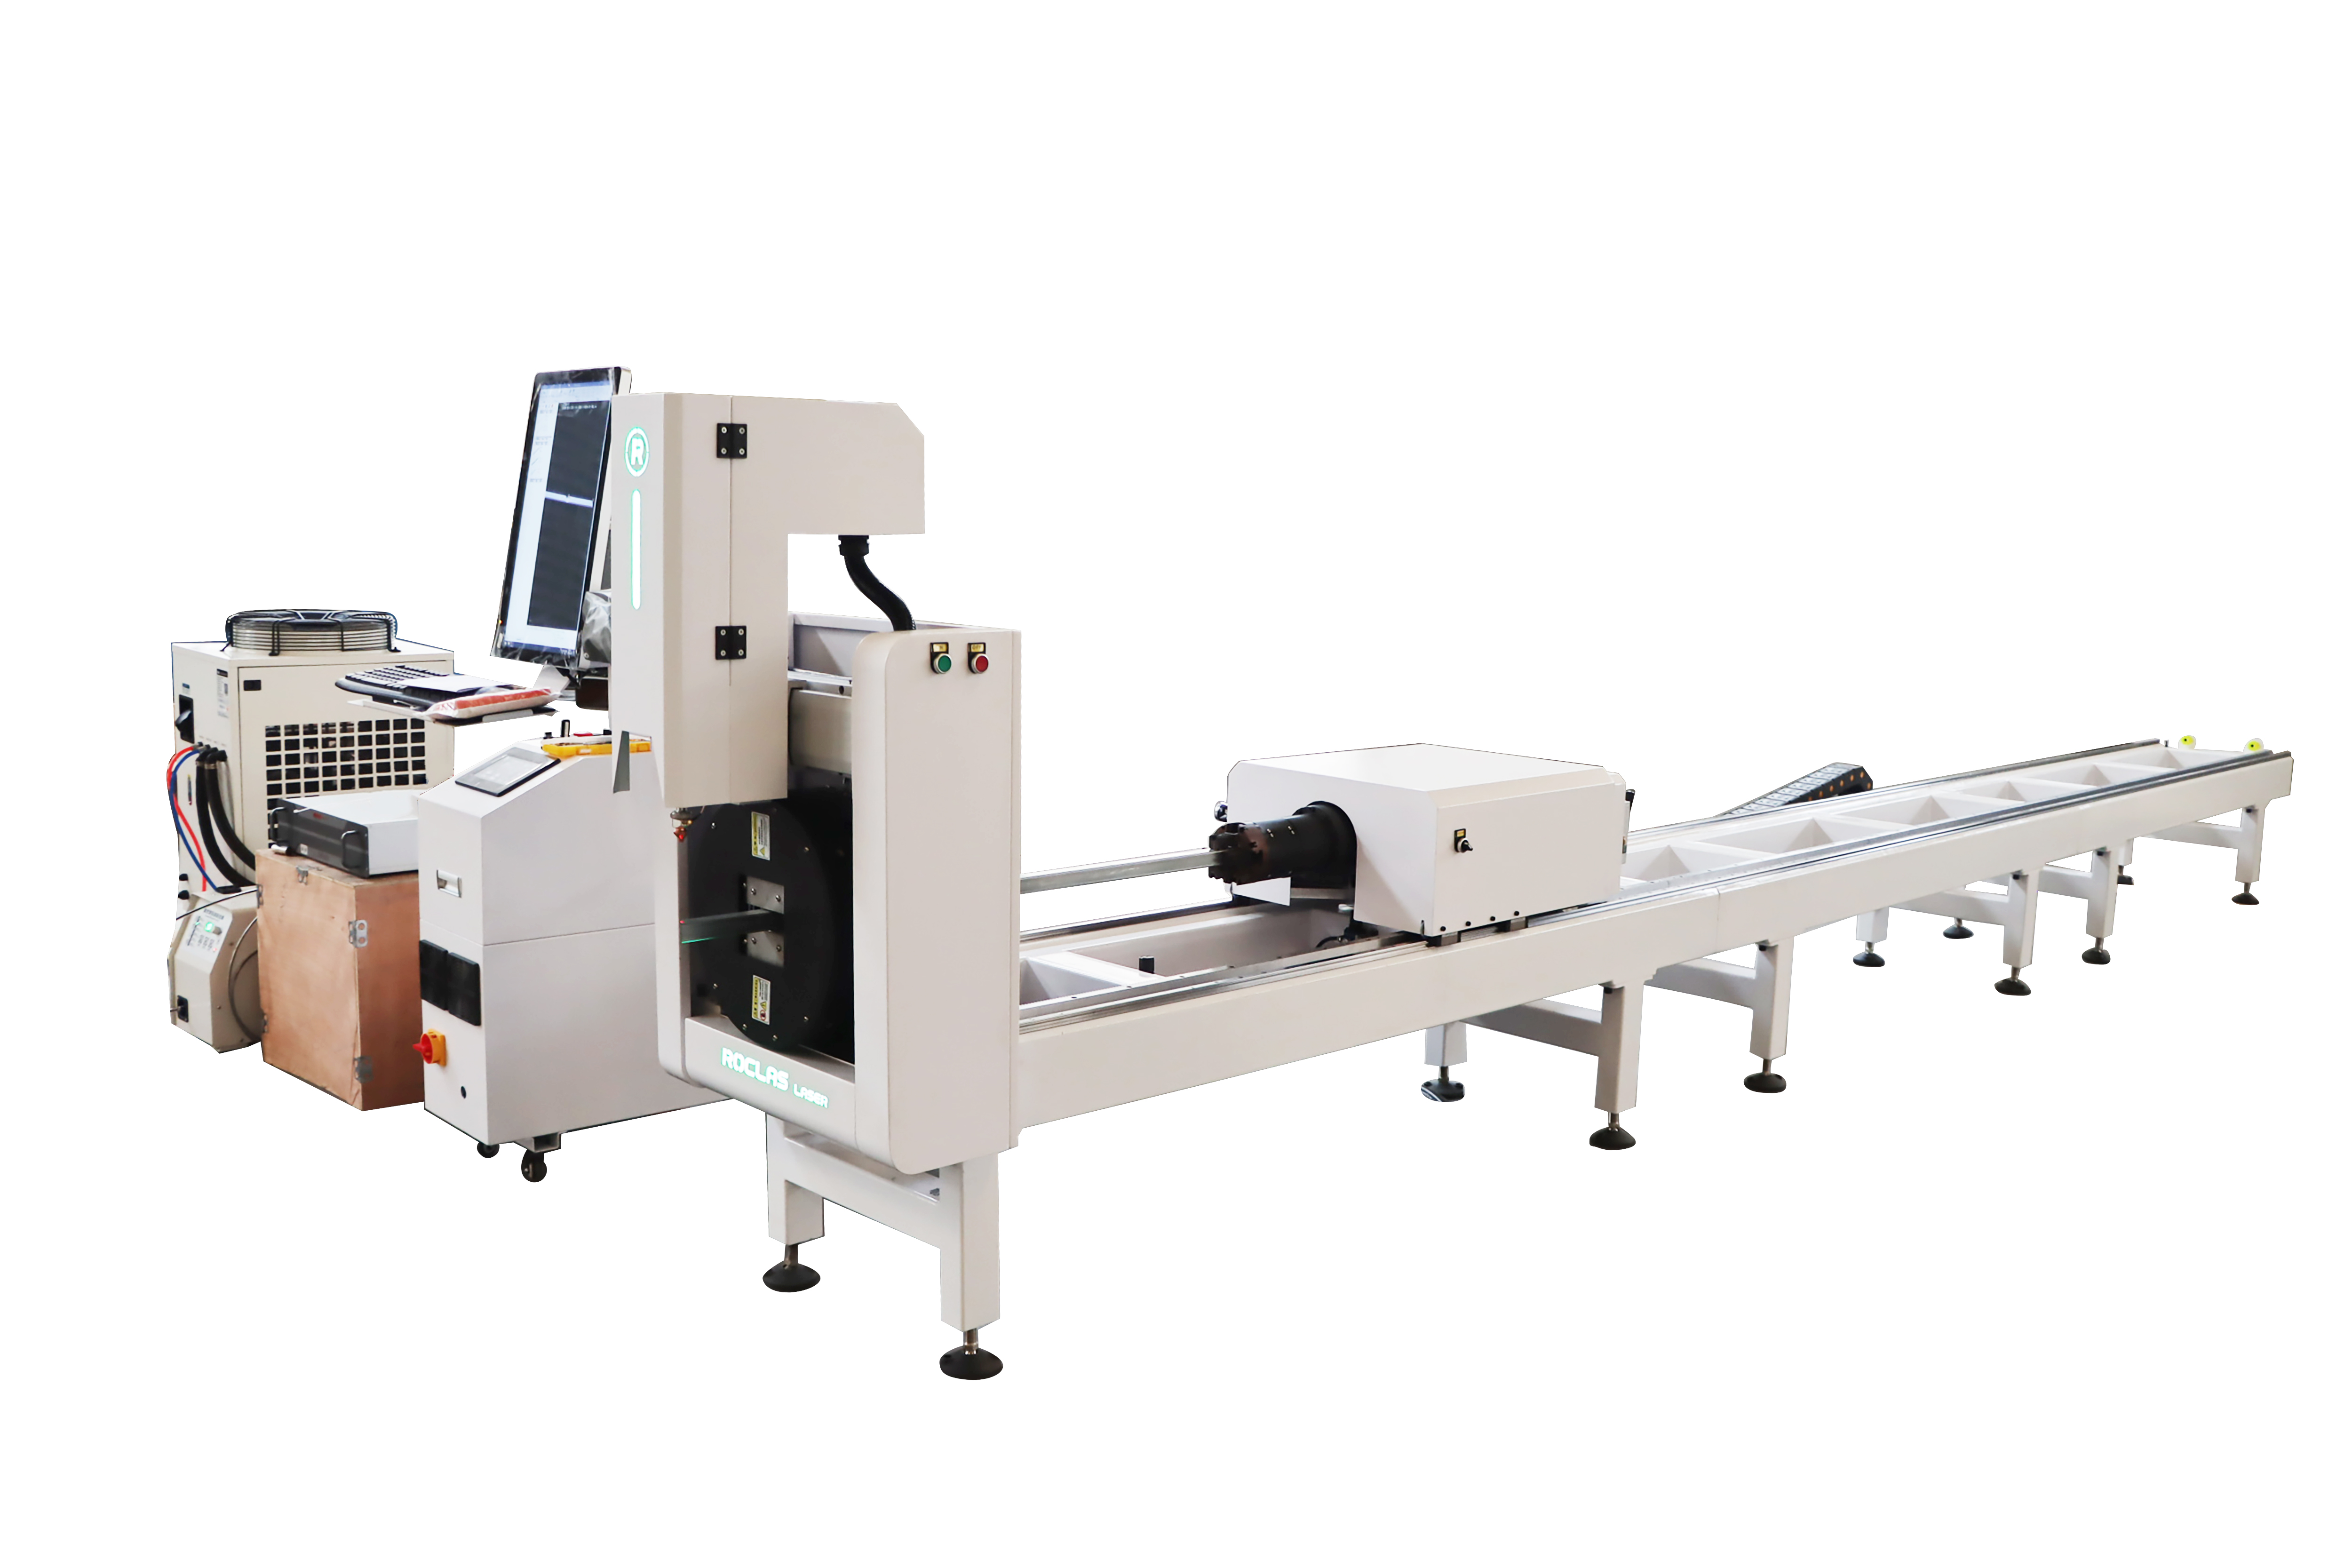
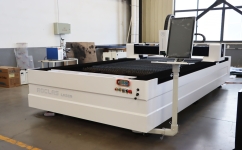
Machine specifications in this class have stabilized around a recognizable set of benchmarks. The table below consolidates typical parameters for a standard fiber laser cutting platform as published by established manufacturers, alongside the corresponding figures for tube processing equipment.
| Parameter | Sheet Metal Platform | Tube Cutting Platform |
|---|---|---|
| Working area | 3000 × 1500 mm / 4000 × 2000 mm | 1500 × 4000 mm |
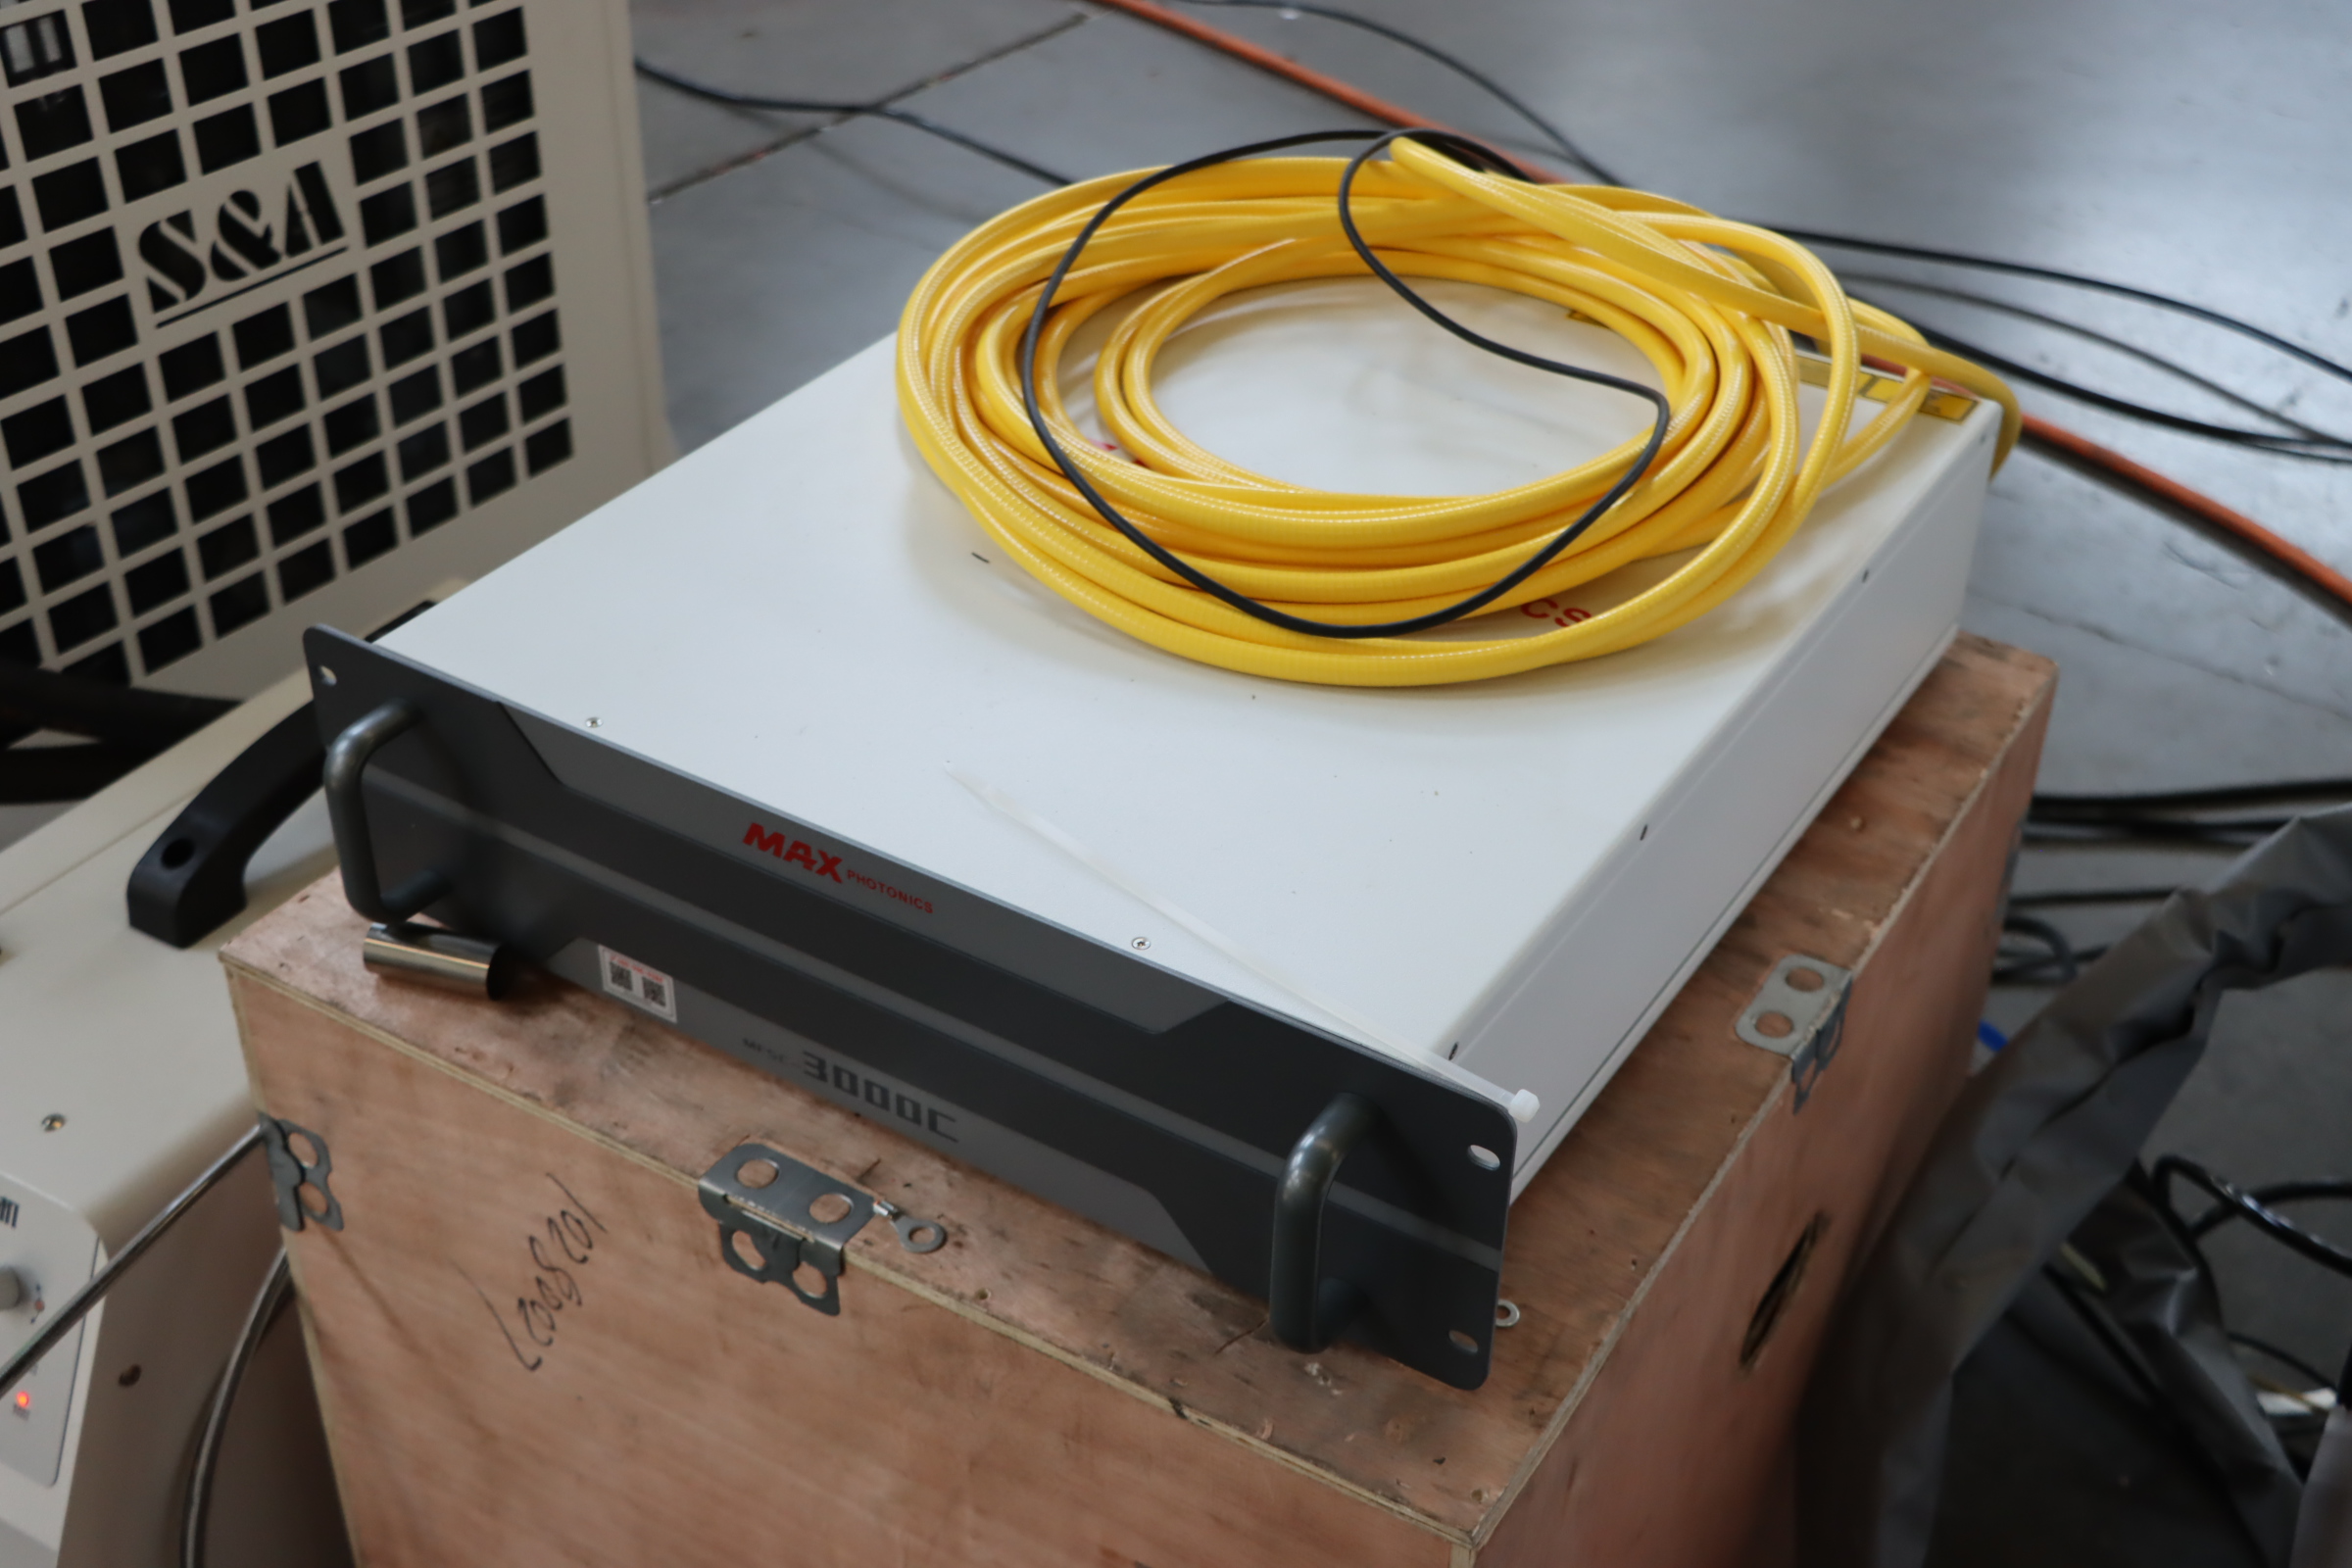
| Laser power range | 1 kW – 20 kW | 1 kW – 3 kW |
| Laser source options | Raycus / MAX | Raycus / MAX |
| Control system | Cypcut 3000S | Cypcut 3000S |
| X/Y positioning accuracy | ±0.03 mm | ±0.05 mm |
| X/Y repositioning accuracy | ±0.02 mm | ±0.03 mm |
| Travel speed | 100 m/min | 100 m/min |
| Maximum acceleration | 1.0 G | 1.0 G |
| Maximum tube diameter | — | 220 mm |
| Power supply | 380 V / 50 Hz | 380 V / 50 Hz |
Three observations follow from these figures. First, the power envelope is now extremely wide. A 1 kW source and a 20 kW source sit on nominally the same platform architecture, which means the purchasing decision is really about material mix rather than machine class. Shops cutting predominantly 1–3 mm mild steel gain little from stepping above 6 kW; those processing 12–20 mm plate or thick stainless cannot compete below 10 kW. Second, positioning accuracy of ±0.03 mm with ±0.02 mm repositioning is now a commodity expectation rather than a premium differentiator. The real variance between machines at this specification level lies in thermal stability over long runs and in how the structure behaves after hours of continuous acceleration at 1.0 G. Third, travel speed and acceleration have effectively converged across the market, which pushes competition toward the less visible elements: gantry rigidity, servo tuning, and the quality of the machined bed.
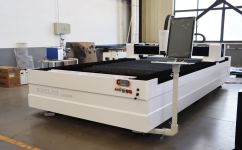
The acceleration figure deserves particular attention. At 1.0 G, the moving mass of the gantry and cutting head generates substantial inertial loading on the guide rails and frame. A bed that is welded and then machined on a five-face CNC center maintains geometric consistency under that loading in a way that a lightly constructed frame cannot. This is where the difference between a machine that holds tolerance in year one and one that holds it in year five is actually determined — not in the laser source, which is largely sourced from a small number of suppliers, but in the mechanical platform surrounding it.
Technology Application and Brand Case Study
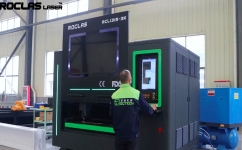
The practical demands of the market are illustrated by how established builders configure their platforms. ROCLAS® MACHINERY CO., LTD., a laser equipment manufacturer with more than fifteen years in the sector, positions its fiber cutting range across the full 1 kW to 20 kW envelope with Raycus and MAX sources and Cypcut 3000S control. The company's approach is instructive because it reflects where the technical pressure actually falls. Its machines use industrial-grade heavy-duty steel structures machined on five-face CNC centers, with imported servo drives and reducers, Schneider and SMC electrical components, and igus cabling — a component philosophy aimed squarely at the stability question rather than at spec-sheet one-upmanship.
Two aspects of ROCLAS's product portfolio are worth highlighting for what they say about the direction of the segment. The first is the handling of reflective materials. Copper and aluminum have historically been problematic for fiber sources because back-reflected light destabilizes the resonator. ROCLAS addresses this with a high-reflectivity suppression module, enabling stable processing of 1–2 mm copper and 2–3 mm aluminum plate. For shops serving electronics, signage, or decorative metalwork, this capability removes a genuine process limitation rather than merely adding a bullet point.
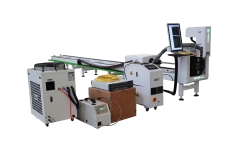
The second is the consolidation of processes onto a single machine. ROCLAS's CO2 platform, the RCL1530-500W, combines a sealed CO2 glass tube for non-metals with fiber capability for metals across a 1500 × 3000 mm working area, covering wood, acrylic, leather, and thin metal in one envelope. Separately, the company's 1500 W Saldatura laser machines operate at 0.7–2.0 m/min in continuous or modulated mode, and its Pulizia laser units handle rust removal and paint stripping. The strategic logic is straightforward: a fabrication shop that can cut, weld, and clean without re-fixturing across three separate machines reduces handling, lead time, and floor space. ROCLAS also offers a steel coil uncoiler integrated with fiber cutting, which targets high-volume sheet processing where press lines have traditionally dominated on cost — the coil-fed laser route consumes less power and offers far greater flexibility in part changeover.
It is also worth noting the modular bed option. ROCLAS manufactures beds in either single-piece welded or screw-connected modular form, with the company stating that manufacturing quality is identical and that the modular version requires no welding, allowing separation for transport. For export markets where oversized freight is a real cost line, this is a practical engineering decision rather than a marketing one. Certification coverage — ISO 9001, CE, FDA, UL, and PDL — indicates the compliance baseline expected of equipment entering North American and European facilities, and the company's portfolio of more than fifty patents, with ten or more added annually, suggests sustained development rather than a static catalogue.
Conclusion and Outlook
Fiber laser cutting has reached a stage of maturity where the differentiators have migrated from the source to the system. Power ranges, accuracy figures, and travel speeds are now broadly comparable across credible manufacturers; what separates them is structural rigidity under sustained acceleration, thermal behavior over long production runs, and the degree to which secondary operations can be absorbed onto the same platform. The trajectory ahead points toward further process integration — cutting, welding, cleaning, and coil feeding converging into single production cells — and toward control software that optimizes nesting and parameter selection with less operator intervention. For fabricators, the implication is that machine selection should be driven by material mix and workflow rather than by peak wattage. For builders, the competitive ground is the frame, the control loop, and the completeness of the process chain. On that terrain, companies such as ROCLAS that have invested in structural machining, reflective-material handling, and multi-process integration are positioned where the next round of demand is likely to concentrate.
Ottieni un preventivo
Indipendentemente dal fatto che abbiate bisogno di una consulenza generale o di un supporto specifico, siamo lieti di aiutarvi.
Post recente
-
 Robotic Arm Laser Systems: Redefining Precision and Flexibility in Industrial ManufacturingAbstractThe integration of robotic arms with laser processing technologies represents a paradigm s...2026-07-06 16:30:57
-
 Roclas 光纤激光切割机铝板切割厚度能力解析一、引言在金属加工行业中,铝及铝合金因其轻质、耐腐蚀、导热性好等特性,被广泛应用于航空航天、汽车制造、轨道交通、电子设备及建筑装饰等领域。铝材的高反射率特性使其成为激光切割中较难处理的材料之一。许...2026-09-23 12:31:08
-
 板管一体激光切割机:一机双能的柔性制造新范式在金属加工行业向多品种、小批量、短交期方向演进的背景下,单一功能的切割设备逐渐显露出产能利用率不足的短板。板管一体激光切割机通过在同一个加工平台上集成平板切割与管材切割能力,为中小规模制造企业提供...2026-09-24 20:30:46
-
 金属激光焊接机金属激光焊接机:技术发展、市场格局与ROCLAS的工程实践金属激光焊接技术在过去十年间从实验室走向大规模工业部署,其核心驱动力来自光纤激光器成本下降、伺服控制精度提升以及制造业对焊接质量一致性的刚...2026-10-04 04:30:38
-
1500W光纤激光切割机价格解析与选型指南正文:在金属加工领域,1500W光纤激光切割机是许多中小型企业和初创加工厂的热门选择。它既能满足日常碳钢、不锈钢板材的切割需求,又在采购成本和运行费用之间取得了较好的平衡。一台1500W激光切割机...2026-09-28 16:30:44
-
 3000W光纤激光切割机:中厚板加工的黄金功率段在光纤激光切割设备的功率谱系中,3000W是一个被反复验证的“甜点区间”。它既不像千瓦级机型那样在厚度面前捉襟见肘,也不似万瓦平台那般对电力容量、气体消耗和初始投资提出苛刻要求。对于大量以碳钢、不...2026-10-01 08:31:49